

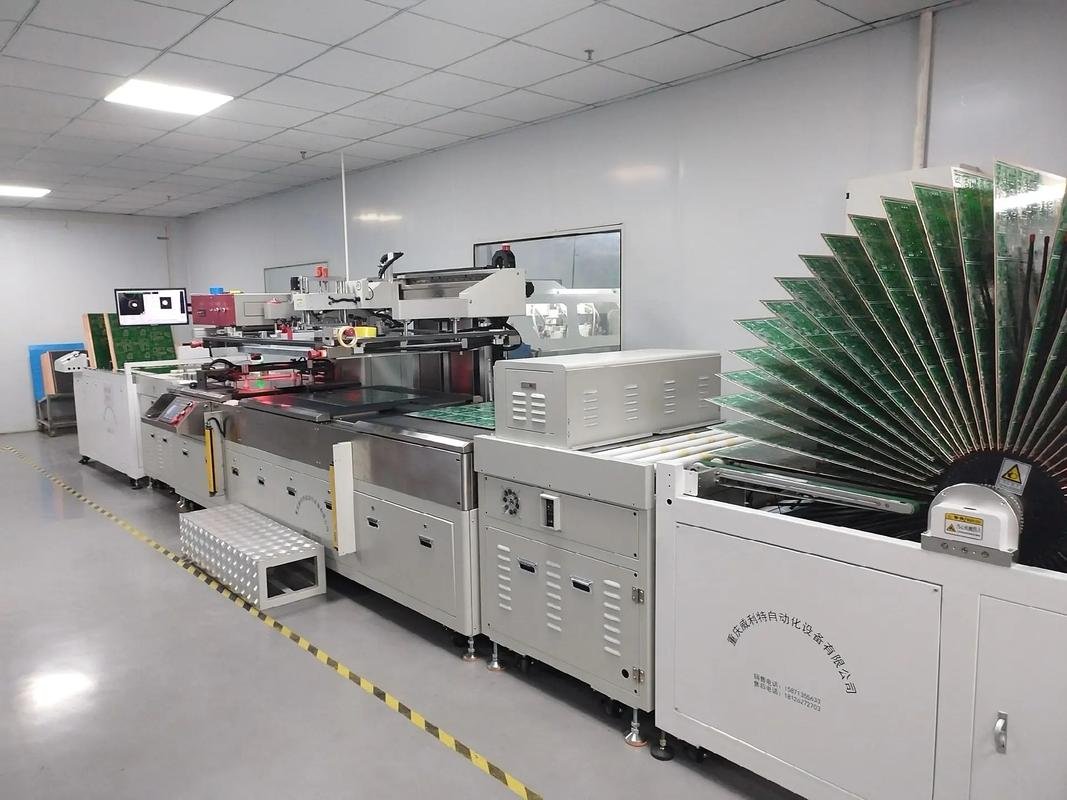
Most solder defects are created before a single component is placed. Insufficient paste causes opens; excess causes bridging; misalignment causes tombstoning and skew. Solder paste inspection is the only in-line check that sees these defects while they can still be fixed — the board can be cleaned and reprinted instead of scrapped.
This article explains what SPI measures, what tolerances are meaningful, how paste handling affects the result, and — critically — what SPI does not cover, so you can specify the right inspection chain rather than assuming one step does everything.

What Is Solder Paste Inspection?
Five measurements per pad
SPI is an optical measurement of the solder paste deposit immediately after stencil printing and before component placement. A typical system projects a structured light pattern onto the paste and reconstructs its three-dimensional shape, pad by pad.
It measures, for each pad:
- Volume — the total amount of paste
- Height — the peak thickness
- Area — the deposited footprint
- Offset — displacement relative to the pad centre
- Shape defects — bridging between pads, slumping, missing deposits
The output is a pass/fail decision per pad against limits set by the process engineer, plus data for trend analysis.
Why SPI Comes Before Placement
The sequence matters because paste defects are cheapest to fix at the point they occur.
| Defect | Cause | Consequence if undetected |
|---|---|---|
| Insufficient volume | Clogged aperture, low squeegee pressure, bad stencil | Open joint, weak fillet |
| Excess volume | Large aperture, low stencil gap, paste too thin | Bridging, solder balls |
| Height variation | Uneven stencil, warped board, poor support | Tombstoning, component tilt |
| Offset | Stencil misalignment, board movement | Skew, insufficient fillet on one side |
| Bridging | Excess paste, fine pitch, poor release | Short circuit |
After reflow, cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
| Parameter | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
|---|---|
| Volume | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| Height | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| Area | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| Offset | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| Bridging | Zero tolerance between adjacent pads |
Two points buyers should understand:
Tighter limits cost money. A 50–150% window passes boards a 70–130% window would reject. Screening more boards means more reprints, more cleaning and more time.
The limits must match the package. A 0402 passive and a 0.4 mm pitch QFN do not share the same tolerance. A specification that applies one limit to the whole board is either over-screening the coarse parts or under-screening the fine ones.
Is Solder Paste Hazardous?
Yes, and the hazard depends on the alloy.
Lead-free paste (SAC305 and similar) contains tin, silver and copper powder in a flux vehicle. It is not "safe because it is lead-free" — the flux is a skin sensitiser and respiratory irritant, and fine metal powder is a dust hazard. Handling requirements include gloves, ventilation and dust control.
Leaded paste (Sn63Pb37) adds lead toxicity, which brings additional regulatory and disposal requirements. Most commercial assembly has moved to lead-free, but leaded paste still appears in high-reliability and aerospace work.
The practical controls at an assembly house: refrigerated storage, controlled warm-up to room temperature before use, a defined open-time and working-life window, and disposal of expired paste rather than re-use. Poor paste handling produces defects that look like process failures.
How Do You Check Solder Paste Quality?
Four checks, in order:
- Storage and warm-up. Paste is stored cold and must reach room temperature before opening, or condensation introduces moisture. Using cold paste causes spattering and voids.
- Viscosity and consistency. Paste that is too thick does not release from the stencil; too thin slumps and bridges. The supplier's handling window is the reference.
- Powder size versus pitch. Type 3, 4 and 5 powders are used for progressively finer pitch. Using Type 3 on a 0.4 mm pitch device gives inconsistent deposits.
- Time and environment. Open time, working life, room humidity and stencil cleaning frequency all affect print quality. These are process parameters, and they should be documented in the assembly house's process control plan.
SPI measures the result of all four. If SPI rejects are consistently high, the cause is usually in one of them.
What SPI Does Not Do
Six checks, and the blind spot in each
This is the part buyers most often get wrong.
| Check | What it covers | What it misses |
|---|---|---|
| SPI | Paste deposit, before placement | Component placement, joint formation |
| Pre-reflow AOI | Placement position and orientation | Joint quality (no joint yet) |
| Post-reflow AOI | Visible joints, missing or wrong parts, polarity | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| X-Ray | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
| FCT | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits | cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits |
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits. cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
For a BGA design, X-Ray belongs in the specification. For a product with functional requirements, FCT belongs in the specification. Each is a line item, and each is cheaper to define up front.
How to Specify Inspection in an Order
- State the package mix — fine pitch, BGA, QFN, 01005 — so the supplier can set the right SPI limits.
- Ask for SPI on fine-pitch and area-array boards explicitly. It is standard in capable houses but not universal.
- Specify X-Ray for hidden joints, with the acceptance criteria for voids if they matter to your application.
- Specify ICT or FCT if function matters, with pass criteria.
- Ask for the inspection report, not just a pass statement.
- Agree the disposition rule for rejects — reprint, rework or scrap, and who pays.
Where Buyers Get SPI Wrong
Assuming SPI is universal. Some houses print without measuring. On fine-pitch work, that is a quality gap, not a cost saving.
Assuming SPI covers placement. It runs before placement. It cannot see a rotated component.
Applying one tolerance to the whole board. Fine pitch needs tighter limits than coarse passives.
Ignoring paste handling. The best SPI system cannot fix paste that was used cold or past its working life.
Assuming AOI replaces X-Ray. AOI sees surfaces. BGA joints are under the package.
Treating inspection as free. SPI, AOI, X-Ray, ICT and FCT each add time and cost. The right approach is to specify what the product's risk justifies.
Checklist
- Confirm the package mix and identify fine-pitch and area-array parts.
- Require SPI where fine pitch or BGA is present, with limits matched to the package.
- Require X-Ray for hidden joints, with void acceptance criteria if relevant.
- Specify AOI coverage: pre-reflow, post-reflow, or both.
- Specify ICT or FCT if function matters, with pass criteria.
- Ask about paste storage, warm-up and working-life control.
- Ask for inspection reports with the shipment.
- Agree the reject disposition rule before the build.
よくある質問
Is SPI necessary on every assembly order?
Not on every order, but on every board with fine pitch or area-array packages. Coarse through-hole and 0805 work can be controlled by print parameters and visual checks. Once the pitch gets small, paste volume becomes the dominant defect cause and the only place to catch it cheaply is before placement.
What does SPI reject actually mean?
That a pad's paste deposit fell outside the process window — too little, too much, offset, or bridged. A reject is not a defective board; the board can usually be cleaned and reprinted. What matters is the reprint rate and its trend, because a rising reject rate points to a process problem rather than to individual boards.
Can SPI replace AOI?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
Why YC PCB
- 20+ years of PCB and PCBA manufacturing, exporting to 20+ countries
- cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
- cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
- SMT, THT/DIP and mixed-technology assembly in-house
- BOM management and component sourcing, with alternates confirmed before build
- DFM/DFA review before production; NDA available for customer IP
- ISO 9001 and UL certification; RoHS compliance documentation on request
Get a Quote cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.


 Japanese
 English
 French
 German
 Spanish
 Italian
 Portuguese
 Russian
 Dutch
 Turkish
